NINVA 凝华北京凝华科技有限公司

ELECTROSTATIC CHUCK

Electrostatic chucks process and equipment solution

Electrostatic-chuck manufacture connects plate geometry, helium holes and gas passages, mating features and functional-surface microfeatures. Establish reusable plate datums, coordinate hole making, surface finishing and microfeature machining, then verify the complete part through dimensional, surface, cleanliness and functional records. NINVA equipment combinations cover grinding, suitable laser features and wheel preparation.

Aluminum nitride · AlNAlumina · Al₂O₃

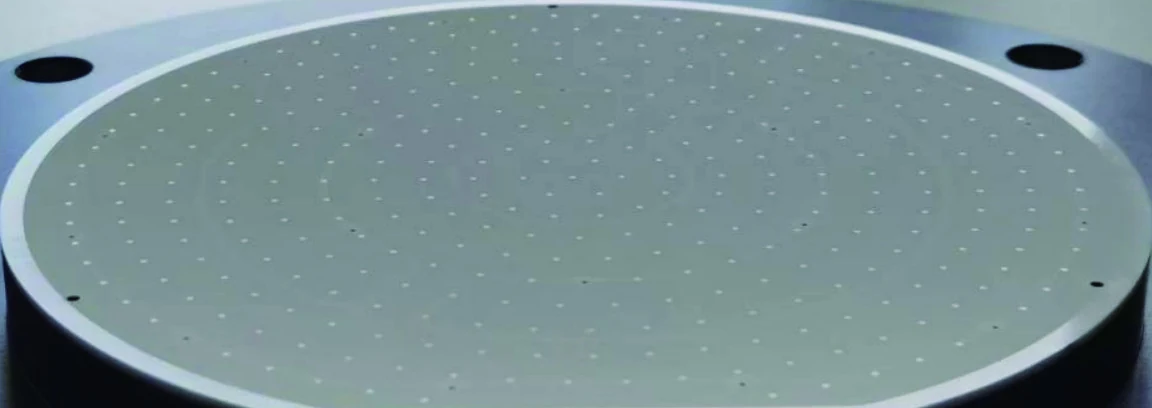
Typical bump features

Bump diameter
1 mm / 0.8 mm
Machining depth
10 μm
Explore all part solutions
Electrostatic chucks

DRAWING REQUIREMENTS

Translate drawing requirements into process targets.

Drawing requirement examples

Use these examples to define selection and validation criteria. Confirm actual targets against the customer drawing, material and inspection method.

Flatness
≤30 μm
Parallelism
≤10 μm
Thickness tolerance
±0.05 mm
Working-surface roughness
Ra <0.4 μm
Helium-hole straightness
≤0.05 mm

Inputs for the process solution

Material & incoming condition
Provide the material grade, as-sintered dimensions, stock allowance and surface condition.
Plate geometry
Define flatness, parallelism, thickness and the inspection datums.
Surface features
Specify the size, pattern, depth and edge requirements of bumps and grooves.
Holes & tool access
Provide hole diameters, depths, locations and the available access after workholding.
Inspection & output
State the surface requirements, inspection method, target cycle time and batch size.

MACHINING CHALLENGES

Identify the challenge. Define the process control.

01

Relate plate geometry to workholding condition

Support, clamping and reversal change the machining and inspection condition of a thin plate. Define support positions, clamping and inspection datums together, recording surfaces, thickness and datum relationships both in the setup and after release.

02

Balance removal allowance and protected structures

Rough/finish grinding, hole making and subsequent lapping or polishing share the available removal allowance. Where embedded structures are present, obtain the protected regions and permitted machining envelope from the customer, then allocate allowances and reinspection points to each operation.

03

Align helium passages with surface microfeatures

Helium holes, gas grooves, bumps and sealing or mating regions need defined positional relationships. Review machining direction, access and entrance/exit requirements for holes and grooves before defining the microfeatures relative to them.

04

Coordinate finishing and microfeature sequence

Material removal in a later operation can affect earlier features. Coordinate working-surface finishing, bump or groove machining, any required post-treatment and inspection against the drawing, defining the geometry and surface condition to preserve at every handover.

05

Validate the whole part beyond one local sample

A surface-bump sample documents only its material and feature conditions. Whole-part acceptance must also cover plate geometry, passages, microfeatures, cleanliness and customer-specified functional items, linked to one drawing revision and sample identifier.

COMPLETE PROCESS CHAIN

From incoming part to final acceptance.

Sintered blank & allowance → datum/plate grinding → contours & grooves → helium holes/passages → surface finishing → microfeatures → cleaning & part acceptance

NINVA machine operationsCustomer / supporting process interfaces
  1. 01Prepare the blank & allocate stock
  2. 02Datum establishment & rough/finish plate grinding
  3. 03Grind profiles & accessible hole or groove features
  4. 04Lapping, polishing & CMP finishing
  5. 05Clean & transfer between operations
  6. 06Dimensional & functional acceptance
  1. 01
    Customer / supporting process interface

    Prepare the blank & allocate stock

    Allocate machining stock against the incoming material, formed condition and subsequent operations, with traceable locating and handling identification.

    Purpose
    Use incoming condition, allowed removal and protected regions as the common input to all downstream operations.
    Operation output
    A prepared blank and stock-allocation record
    Inspection items
    Check material, incoming dimensions, surface condition and stock on each functional surface.
    Handover conditions
    Transfer material/blank identification, drawing revision, initial dimensions and face-specific allowance, with protected regions identified.
  2. 02
    Operation supported by NINVA equipment

    Datum establishment & rough/finish plate grinding

    Organize rough and finish grinding around plate geometry, thickness and reversal datums, allocating removal at each stage. The NHM configuration must account for the part, support fixture and tooling, with plate results recorded in agreed workholding and inspection conditions.

    Purpose
    Create plate and reversal datums before holes, grooves and microfeatures require a shared location reference.
    Operation output
    Plate surfaces and datums for subsequent hole, groove and microfeature operations
    Inspection items
    Inspect plate geometry, thickness and datum relationships after setup changes.
    Handover conditions
    Transfer plate, thickness and reversal-inspection records together with the locating surfaces to use downstream.
  3. 03
    Operation supported by NINVA equipment

    Grind profiles & accessible hole or groove features

    Grind external profiles, steps, mating features and accessible holes or grooves from the preceding datums. Define a separate route for deep microholes.

    Part, fixture and tool space must fit the selected model.

    Purpose
    Use established plate datums to create contours and mating features, giving passages and functional surfaces a defined interface.
    Operation output
    Mechanically machined profiles and mating features
    Inspection items
    Inspect feature dimensions, positions, edges and their relationship to the plate datums.
    Handover conditions
    Transfer contour, step, groove and passage datum relationships, edge inspection and remaining finishing allowance.
  4. 04
    Customer / supporting process interface

    Lapping, polishing & CMP finishing

    Coordinate the customer’s existing or supporting lapping, polishing or CMP operations against the working-surface drawing, defining surface and stock relationships before and after microfeature machining.

    Select the finishing method and operation sequence through validation of the material, working-surface requirements and customer process.

    Purpose
    Plan geometric and surface finishing against the working-surface requirements, coordinating retained allowance with microfeature machining.
    Operation output
    A working-surface base meeting the requirements of this stage
    Inspection items
    Inspect plate geometry, roughness and surface condition using the agreed methods.
    Handover conditions
    Transfer finished plate/surface records and define the permitted pre-/post-microfeature condition and post-treatment scope.
  5. 05
    Customer / supporting process interface

    Clean & transfer between operations

    Connect mechanical and surface operations to the customer’s or supporting operations’ cleaning, drying and handling procedures.

    Purpose
    Connect surface and passage machining with cleaning and transfer requirements before assembly.
    Operation output
    A cleaned component handled according to subsequent assembly requirements
    Inspection items
    Check cleanliness, appearance and handling records against the customer specification.
    Handover conditions
    Transfer cleaning-batch, visual and cleanliness records, drying and packaging/handling conditions to the customer specification.
  6. 06
    Customer / supporting process interface

    Dimensional & functional acceptance

    Link operation records and geometric inspection with the customer’s subsequent assembly or functional tests, keeping component acceptance and machine delivery acceptance distinct.

    Purpose
    Assess local machining results together against the complete drawing and customer functional specification.
    Operation output
    Traceable component acceptance and process records
    Inspection items
    Complete acceptance against the component drawing, inspection plan and customer functional specification.
    Handover conditions
    Transfer dimensional, passage, microfeature, surface and applicable functional-acceptance records under the same part identifier.

FEATURE-SPECIFIC ROUTES

Additional operations selected for the material and geometry

Conditional route 01

Helium-hole & gas-passage machining

For drawing-defined helium holes, gas passages or special deep holes, coordinate customer or supporting hole-making equipment and processes. Select the route against diameter, depth, straightness and entrance/exit requirements; an LTC400 surface sample does not establish deep-hole capability.

Select where the drawing includes helium holes, passages or other dedicated hole-making requirements.

Purpose
Relate passages to the plate, contours and functional regions before handing over their condition to surface and microfeature operations.
Operation output
Identified hole/passage features referenced to common datums
Inspection items
Inspect diameter, position, depth/patency, entrance/exit integrity and customer-specified passage criteria.
Handover conditions
Transfer hole/passage identifiers, machining direction, inspection records and openings requiring protection or avoidance.
Conditional route 02

Laser-machine working-surface microfeatures

Assess the LTC400 for bumps, grooves and other surface features in suitable ceramics, using the prepared working surface and locating datums. The chuck bump sample informs selection for this operation only.

The drawing must contain laser-suitable surface features, with material and base-surface conditions validated.

Purpose
Machine functional microfeatures on a traceable working surface and datum system without extrapolating one sample to whole-part performance.
Operation output
Local surface microfeatures produced under the conditions defined for the part
Inspection items
Inspect feature depth, dimensions, distribution and the post-process surface condition.
Handover conditions
Transfer bump/groove location, actual dimensions/depths, edge and surface records; where gas outlets, sealing bands or mating regions exist, also verify clearance/avoidance relationships.
GRINDING SUPPORT

Wheel production and dressing support component grinding.

Profiled-wheel production & dressing

Where component grinding uses suitable electrically conductive metal-bond diamond or CBN profiled wheels, assess the SL25L / SL30 for wheel-profile production, dressing and worn-profile restoration. This supporting operation acts on the wheel and is coordinated separately with component grinding and measurement results.

EQUIPMENT COMBINATIONS

Combine equipment around the machining task.

01

Plate & structural grinding combination

For plate, contour and mating-feature work where the customer already has passage making, finishing or cleaning processes.

NINVA equipment and roles

Component grinding: select the machine size against part, support fixture and tool space; establish plate and reversal datums.

Supporting wheel line: produce, dress or restore profiles only for suitable electrically conductive metal-bond profiled wheels.

Customer and supporting operations

  • Coordinate helium passages, subsequent lapping/CMP, cleaning and functional acceptance through existing or project-supporting processes.

Combination validation priorities

  • Validate support/clamping, reversal datums, allowance and inspection condition to establish actual machine coverage.
  • Link wheel condition to plate and structural inspection records.
02

Grinding & surface-microfeature combination

For plate/structure work plus bumps, microgrooves or local engraving on a suitable ceramic working surface.

NINVA equipment and roles

Establish plate geometry, mating features and common location references.

Microfeature branch: machine validated local surface features in coordination with prior finishing and subsequent treatment.

Provide independent profile production and dressing for applicable grinding wheels.

Customer and supporting operations

  • Dedicated hole making, lapping/CMP, cleaning and whole-part functional acceptance remain customer or supporting process interfaces.

Combination validation priorities

  • Validate bump/groove dimensions, depth, edges and working-surface condition on the actual material.
  • Confirm plate geometry separately from local microfeatures; do not combine them into unvalidated whole-part performance.
View the function and conditions of each machine type

For structural grinding of hard and brittle materials, select the size against the plate, workholding and tool space. In-process measurement and other options are specified for the selected model.

For surface engraving, shaping and cutting, with the existing alumina electrostatic-chuck surface-feature sample available to inform validation.

Where profile grinding requires a shaped wheel, assess production and dressing of the wheel profile for suitable electrically conductive metal-bond wheels.

VALIDATION & HANDOVER

Connect the process chain through inspection and handover records.

Validation itemInspection methodHandover record
Plate geometry & thicknessUse agreed drawing datums, supports and inspection conditions in the setup and after release.Surface/parallel relationships, thickness, measurement positions and workholding-condition records.
Passage & structural locationInspect helium holes, passages, grooves and mating features by identifier and datum.Diameter, position, depth/patency, opening integrity and datum-link records.
Working-surface microfeaturesSelect positions and features from the drawing; inspect bump/groove dimensions, depths and surfaces separately.Microfeature location map, dimensional/depth results and machining conditions.
Finishing handoverCompare allowed removal and geometry/surface condition before and after lapping, polishing or CMP.Pre-/post-operation inspection, allowance consumption and post-treatment items.
Whole-part & functional itemsThe customer or agreed supporting party performs applicable cleanliness and functional tests to the part specification.Complete acceptance records linked to one drawing revision and part identifier.

Prepare these inputs for the process discussion

  1. Material grade, blank/embedded-structure condition, plate diameter/thickness and face-specific allowances.
  2. Complete drawings and datums for plate surfaces, passages, bumps/grooves and mating regions.
  3. Diameter, depth, straightness relationships, opening direction and edge requirements for helium or other deep holes.
  4. Current process sequence, support/clamping method and principal nonconformity records.
  5. Inspection methods, output/cycle objectives, existing supporting processes and equipment implementation plan.

OPERATION SAMPLE RECORDS

Documented samples for the relevant operation

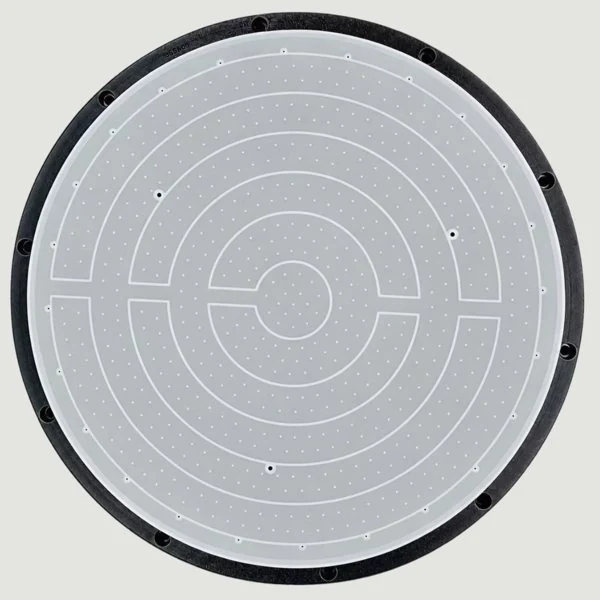
Surface feature machining sample on a 12-inch alumina electrostatic chuck
LTC400

Electrostatic Chuck Surface Feature Machining

Material and workpiece
12-inch alumina electrostatic chuck
Bump depth
15.5 μm±1 μm
Bump diameter
0.85 mm±0.01 mm
View related equipment

VALIDATE YOUR MACHINE SELECTION

Bring the drawing. Define the machine solution.

Share the part, material, critical requirements and output objectives to discuss candidate machines, trials and configuration.

An account manager responds within 24 hours. Trials generally take 3–20 days; an NDA is available.